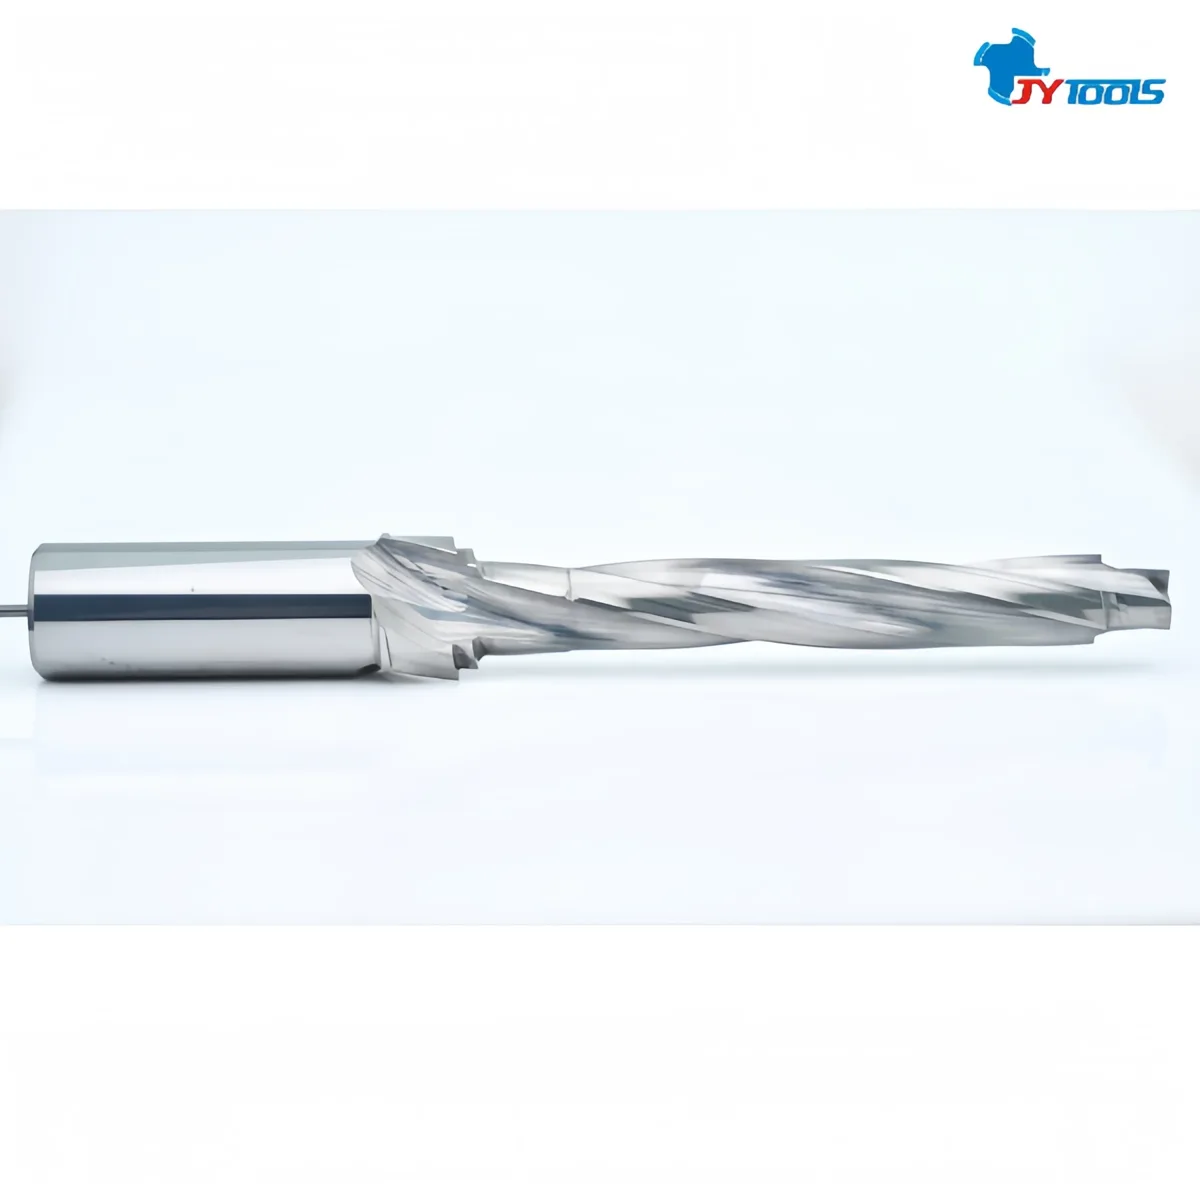
Four-blade reamer / Tapered reamer
The RT730 Series Ultra-Long Helical-Edge Through-Hole Reamers are industry-leading products developed by JIAYI Tools specifically for through-hole machining in ultra-deep holes (20 times the diameter or more) and difficult-to-machine materials. Their innovative "ultra-long helical edge + damping anti-vibration shank" design achieves breakthroughs in "spiral chip evacuation, zero tool vibration, and high surface finish" during ultra-deep hole machining. It completely resolves the industry pain points associated with traditional deep-hole reamers—such as "poor chip evacuation, severe tool vibration, and poor accuracy"—and provides a revolutionary ultra-deep hole machining solution for sectors including aerospace, energy equipment, and mold making.
| Part number | RT730 Series |
|---|---|
| Type | Carbide Reamers |
| Product name | Tapered Helical Reamers / Four-Flute Reamers |
| Coating | Diamond-like (DLC) |
| OEM / ODM | Made to your samples or drawings |
| Origin | Shenzhen, China |
Design details that keep reaming stable, accurate and chatter-free.
The cutting edge is ultra-precisely ground using a five-axis CNC grinding machine, with a runout error of ≤0.05 μm, ensuring that the roundness and cylindricity of the barrel bore are maintained within 0.001 mm, meeting the stringent requirements for military firearms.
The front cutting edge features a 12° guide angle to reduce deformation caused by compression at the entry point; the rear cutting edge incorporates a 0.001 mm finishing edge to ensure a chip-free and burr-free exit, thereby preventing any adverse effects on ballistic stability.
The cutter body is machined from a single piece of ultra-fine-grain cemented carbide (HRC 68) with no welded joints, ensuring no loosening or runout during high-speed, high-feed machining, with a repeatability of ≤0.003 mm.
The tool body is made of WC-Co ultrafine-grain cemented carbide (HRC 70), offering 50% greater chip resistance than standard cemented carbide and capable of withstanding continuous high-intensity machining.
Features a CVD diamond-like coating with a thickness of just 1 μm and a coefficient of friction as low as 0.1. Tool life is three times longer than that of traditional TiAlN coatings, with no risk of coating peeling.
The tool body undergoes cryogenic treatment at -196°C followed by high-temperature tempering to thoroughly eliminate internal stresses, ensuring no deformation or runout during high-speed machining and guaranteeing machining stability.
G1.0-grade dynamic balancing ensures vibration-free operation at high speeds of 30,000 rpm; the shank is made of a damping alloy with built-in micro-damping grooves that absorb over 95% of cutting vibrations. 。
Each reamer passes G2.5-grade dynamic balancing inspection, ensuring vibration-free operation at high speeds of 20,000 rpm and guaranteeing machining stability.
Starting values. Our engineers can tune parameters to your machine and workpiece.
| Workpiece material | Cutting speed vc (m/min) | Feed f (mm/rev) | Coolant |
|---|---|---|---|
| Inconel 718 | 20–40 | 0.02–0.06 | High-pressure internal |
| Stainless Steel 316L | 40–60 | 0.04–0.1 | Internal + MQL |
| Ti6Al4V Titanium Alloy | 30–50 | 0.03–0.08 | MQL |
Typical bores and industries for this reamer.
Machining φ1–φ5 mm ultra-deep through holes in stainless steel and titanium alloy substrates for orthopedic implants and surgical instruments to ensure the precision and biocompatibility of medical devices.
Machining φ4–φ14 mm ultra-deep fluid passages in stainless steel or high-temperature alloy substrates for gas turbines and hydraulic valve blocks to meet the sealing requirements of high-pressure fluid systems.
Machining φ3–φ10 mm ultra-deep holes in titanium alloy and stainless steel substrates for aircraft engine blades and landing gear, with a depth-to-diameter ratio of up to 20:1 and roundness ≤ 0.002 mm.
Machining high-precision holes with diameters ranging from φ4 to φ16 mm in core components of armored vehicles and unmanned aerial vehicles (UAVs) to ensure equipment reliability and service life.
Send your bore size, tolerance and drawing. We manufacture standard sizes and custom reamers made to your samples or drawings.