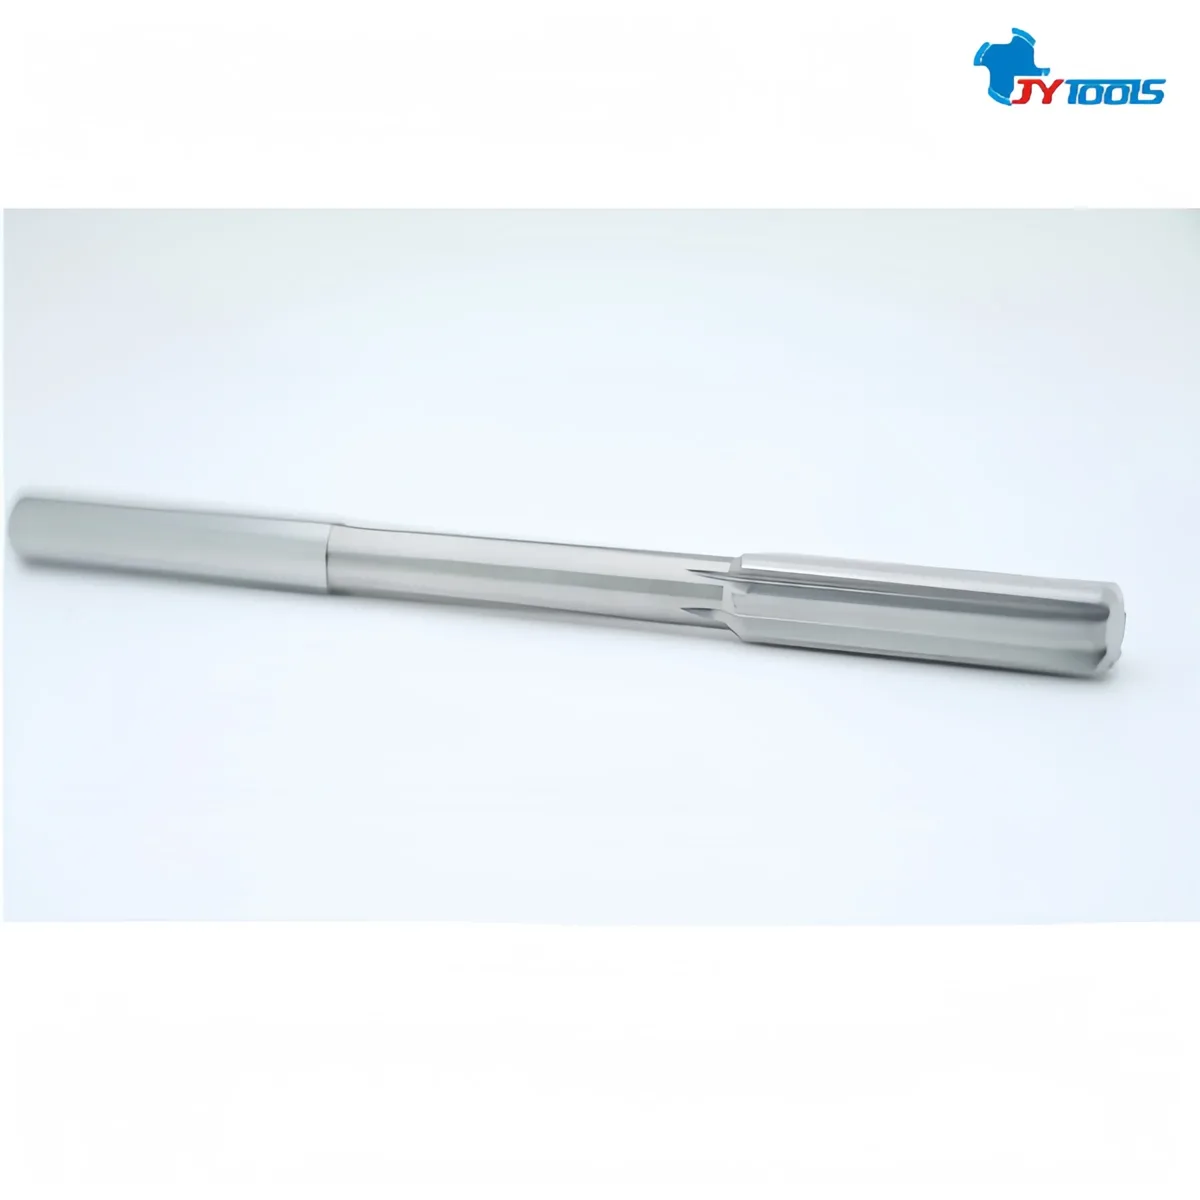
Four-blade reamer / Six-flute straight-groove reamer
The RZ530 Series long-edge through-hole reamers are a breakthrough product line developed by JIAYI Tools specifically for through-hole machining applications requiring extra-long cutting edges and high length-to-diameter ratios. Their innovative "long-edge uniform cutting + zero-step finishing" technology, High-precision machining of through holes with extra-long cutting edges can be completed in a single pass, completely resolving the industry pain points associated with traditional long-edge reamers—such as "uneven cutting, step marks on the hole walls, and chipping at the exit"— It is particularly well-suited for the stringent requirements of ultra-long through-holes in fields such as mold making, hydraulics, and aerospace.
| Part number | RZ530 Series |
|---|---|
| Type | Carbide Reamers |
| Product name | Six-Flute Deep-Hole Reamers/Through-Hole Reamers |
| Coating | Nano TiAlN |
| OEM / ODM | Made to your samples or drawings |
| Origin | Shenzhen, China |
Design details that keep reaming stable, accurate and chatter-free.
Features a 4-flute variable-pitch structure that disrupts the cutting vibration frequency; the edge profile incorporates a 0.002mm tapered + variable-width design, ensuring even force distribution during long-flute cutting and leaving the bore wall free of steps and vibration marks.
The front edge features a 15° guide angle to reduce entry-point deformation; the rear edge incorporates a 0.002 mm mirror-finish edge to ensure no chipping or burrs at the exit, with a consistent hole wall surface roughness of Ra ≤ 0.15 μm.
The tool body is machined from a single piece of ultra-fine-grain carbide (HRC 68) with no welded joints, ensuring no loosening or runout during high-speed, high-feed machining, with a repeatability of ≤0.003 mm.
Utilizing PVD nano-coating technology, the coating is only 2 μm thick, with a hardness as high as HV3800 and a coefficient of friction as low as 0.3, resulting in a tool life twice that of traditional coatings.
Features three built-in helical internal cooling channels with a cooling pressure of up to 120 bar. Combined with a large-capacity chip-carrying groove design, this system increases chip evacuation speed by 50% and prevents chips from scratching the bore wall.
The front edge features a 15° guide angle to reduce entry-point deformation; the rear edge features a 0.002 mm mirror-finish edge to ensure chip-free and burr-free exits, with bore wall surface roughness consistently achieving Ra ≤ 0.15 μm.
The front angle features a 5°–8° adaptive design that automatically optimizes cutting force when machining different materials, reducing tool wear and improving machining stability.
Each reamer passes G2.5-grade dynamic balance testing, ensuring vibration-free operation at high speeds of 20,000 rpm and guaranteeing machining stability.
Starting values. Our engineers can tune parameters to your machine and workpiece.
| Workpiece material | Cutting speed vc (m/min) | Feed f (mm/rev) | Coolant |
|---|---|---|---|
| Aluminum Alloy | 80–120 | 0.08–0.18 | MQL |
| Stainless Steel | 40–70 | 0.05–0.12 | Internal + MQL |
| Steel | 50–80 | 0.06–0.15 | Emulsion |
Typical bores and industries for this reamer.
Machining of φ5–φ20 mm ultra-long-edge guide pillar holes on the base plates of injection molds and stamping dies, with edge lengths up to 150 mm and step-free hole walls to meet the high-precision fit requirements for guide pillars.
Machining of φ4–φ16 mm ultra-long-edge fluid passage holes on the steel base material of hydraulic valve blocks, with edge lengths up to 120 mm, to meet the sealing requirements of high-pressure fluid systems.
Machining φ6–φ25 mm ultra-long-edge connection holes on stainless steel substrates for aircraft landing gear and engine mounts, with edge lengths up to 200 mm and roundness ≤0.002 mm.
Machining of φ2–φ8 mm ultra-long-edge through holes on stainless steel substrates for orthopedic implants and surgical instruments, with edge lengths up to 80 mm, ensuring the precision and biocompatibility of medical devices.
Send your bore size, tolerance and drawing. We manufacture standard sizes and custom reamers made to your samples or drawings.