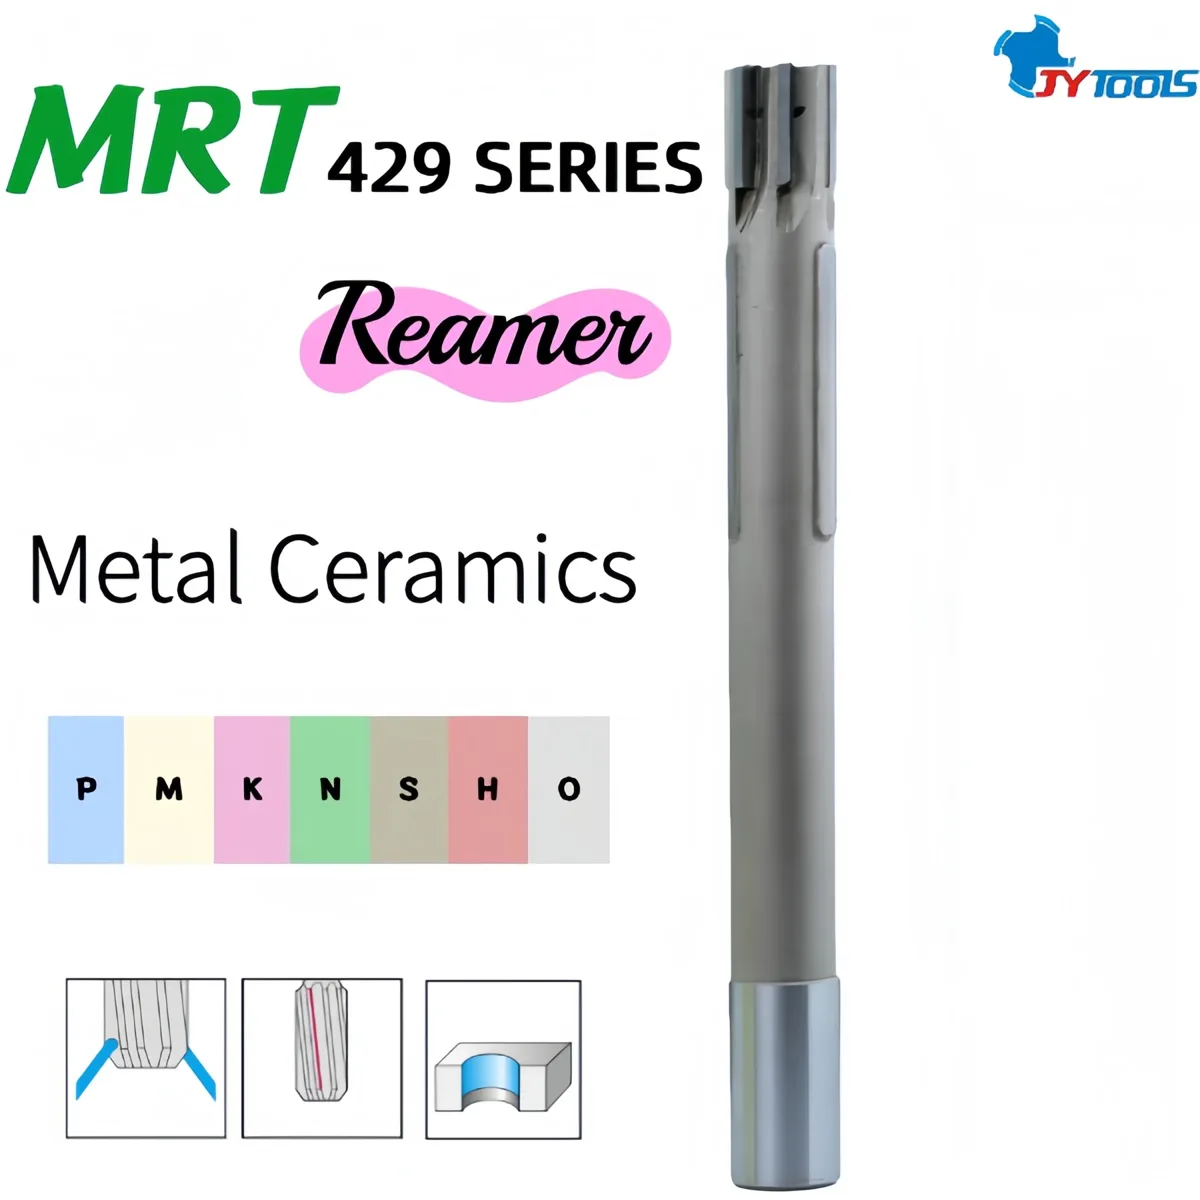
Four-blade reamer
The MRT429 Series deep-hole metal-ceramic reamers are JIAYI Tools’ industry-leading products, specifically designed for precision machining of deep holes with diameters 15 times or more than the tool diameter and high-hardness materials. They feature a nano-metal-ceramic cutting tip Combined with seismic damping shank technology, this innovation has achieved a breakthrough in the deep-hole machining of difficult-to-machine materials—such as quenched steel and stainless steel—by enabling "high-speed cutting, mirror-like finish, and zero chatter," thereby completely resolving the problem of chatter commonly associated with traditional deep-hole reamers, By addressing the pain points of poor precision and short service life, it provides a disruptive deep-hole machining solution for industries such as aerospace, mold manufacturing, and energy equipment.
| Part number | MRT429 Series |
|---|---|
| Type | Brazed Cermet |
| Product name | Deep-hole reamer / Through-hole reamer |
| OEM / ODM | Made to your samples or drawings |
| Origin | Shenzhen, China |
Design details that keep reaming stable, accurate and chatter-free.
Utilizing Ti(C,N)+Al₂O₃ nano-composite ceramics, this formulation achieves a hardness of up to HV4200—30% higher than that of cemented carbide. Additionally, the addition of a WC-Co toughness phase enhances chip-breaking resistance by 40%, making it ideally suited for continuous deep-hole machining of high-hardness quenched steel.
Metal ceramics inherently possess an extremely low coefficient of friction (0.25), eliminating the need for additional coatings to prevent tool sticking. When machining stainless steel and titanium alloys, chips flow smoothly without sticking, and the hole wall surface finish directly achieves a mirror-like finish with Ra ≤ 0.1 μm.
The cutting edge is mirror-polished using a diamond grinding wheel, with a cutting edge radius tolerance of ≤0.001 mm. This ensures no extrusion marks during cutting, and the hole wall surface roughness consistently achieves Ra ≤ 0.1 μm, meeting precision sealing requirements without the need for subsequent grinding.
Features a 6-flute variable-pitch configuration that disrupts the cutting vibration frequency, completely eliminating chatter marks; the cutting edges feature a 0.003 mm taper to reduce friction with the bore wall, further improving bore wall finish.
Features three built-in helical internal cooling channels with a cooling pressure of up to 120 bar. Combined with a large-capacity chip-discharge groove design, this system increases chip evacuation speed by 50% and prevents chips from scratching the bore walls.
The shaft is made of Invar 36, a low-thermal-expansion alloy with a thermal expansion coefficient of only 1.2×10⁻⁶/°C. During high-speed machining, the shaft’s deformation is ≤0.002 mm, ensuring consistent accuracy in deep-hole machining.
The cutting head and shank are joined via a hot-fit interference fit with a fit tolerance of ≤0.001 mm, ensuring no loosening or runout during high-speed, high-feed machining, with a repeatability of ≤0.003 mm.
It maintains a hardness of over 90% even at 1200°C, enabling high-speed machining at vc = 150–200 m/min, with efficiency more than twice that of carbide reamers.
Starting values. Our engineers can tune parameters to your machine and workpiece.
| Workpiece material | Cutting speed vc (m/min) | Feed f (mm/rev) | Coolant |
|---|---|---|---|
| Hardened steel, HRC 45+ | 150–180 | 0.08–0.15 | Internal + emulsion |
| 316L Stainless Steel | 120–160 | 0.06–0.12 | Internal + MQL |
| Ti6Al4V Titanium Alloy | 80–120 | 0.05–0.1 | MQL |
Typical bores and industries for this reamer.
Machining φ3–φ12 mm deep holes in titanium alloy and stainless steel substrates for aircraft engine blades and landing gear, with a depth-to-diameter ratio of up to 15:1 and a roundness tolerance of ≤0.002 mm.
Machining bearing holes with diameters ranging from φ8 to φ25 mm in carburized steel gearbox components with a hardness of HRC 58–62 to meet sealing and precision requirements during high-speed operation.
Machining φ5–φ15 mm deep holes in HRC 55–60 stainless steel landing gear substrates, with a depth-to-diameter ratio of up to 10:1 and a roundness of ≤0.002 mm.
Machining φ4–φ16 mm fluid passage holes in the steel base material of hydraulic valve blocks to meet the sealing requirements of high-pressure fluid systems.
Send your bore size, tolerance and drawing. We manufacture standard sizes and custom reamers made to your samples or drawings.