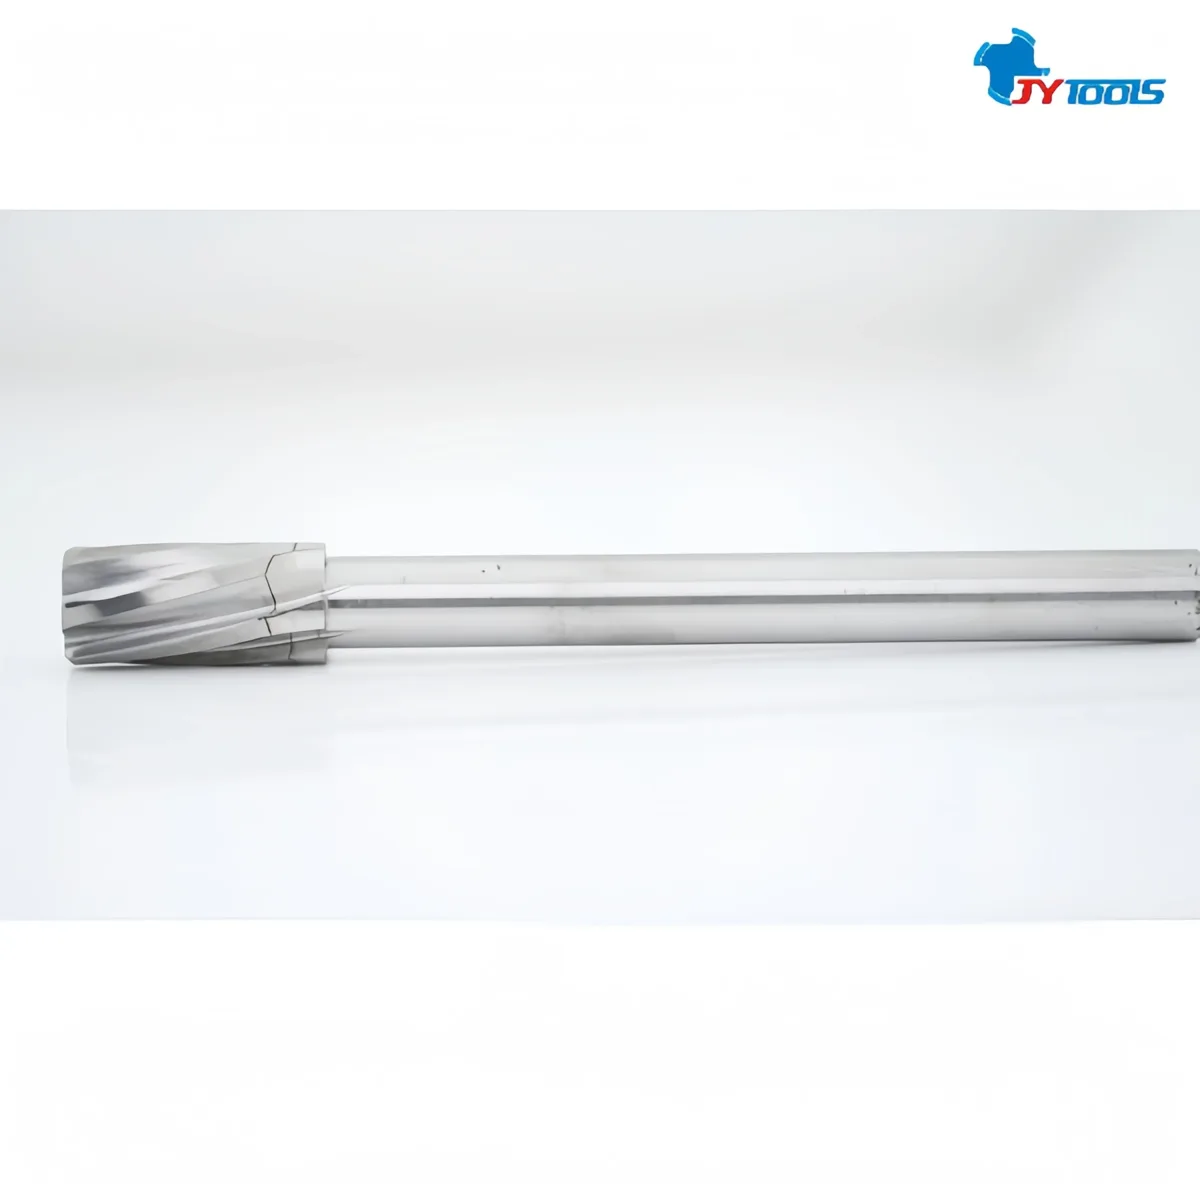
A sharp tool for deep-hole precision reaming
The AR655 V-welded reamer joins a carbide cutting head to a high-strength steel shank with a V-shaped laser weld, solving the breakage and head detachment common in traditional welded reamers. It is built for deep-hole and high-precision bores in aerospace and mold manufacturing.
| Part number | AR655 Series |
|---|---|
| Type | Welded tungsten carbide six-flute reamer |
| Application | Deep-hole / through-hole reaming |
| Example size | D14.75 × 28L × D12 × 186L |
| Coating | Nano TiAlN (PVD, 2 μm) |
| OEM / ODM | Made to your samples or drawings |
| Origin | Shenzhen, China |
Every design detail targets stable, chatter-free reaming in deep and high-tolerance bores.
30% more contact area than flat welding and 50% higher weld strength, withstanding radial impact above 1,000 N.
A 0.005 mm edge taper reduces wall friction, and variable-pitch flutes break up vibration to eliminate chatter marks.
0.002 mm edge passivation prevents chipping and delivers Ra ≤ 0.15 μm for aerospace-grade bores.
Four helical coolant channels at up to 100 bar move chips 40% faster and keep them off the bore wall.
Special damping steel adds 25% rigidity, holding runout to ≤ 0.003 mm at 15× tool diameter.
2 μm PVD coating with hardness up to HV3800 and friction coefficient of 0.3 for twice the tool life.
High-frequency vibration aging removes residual weld stress to prevent cracking at high speed and depth.
Every reamer is ultrasonically tested at the factory to confirm the weld is free of internal defects.
Starting values. Our engineers can tune parameters to your machine and workpiece.
| Workpiece material | Cutting speed vc (m/min) | Feed f (mm/rev) | Coolant |
|---|---|---|---|
| Titanium alloy | 40–60 | 0.05–0.15 | MQL |
| Stainless steel | 50–80 | 0.08–0.20 | Internal + emulsion |
| Steel | 60–100 | 0.10–0.25 | Emulsion |
Proven in bores where precision, depth and surface finish all matter.
Deep holes in titanium engine blade and landing gear components, plus hydraulic and pneumatic control parts.
Micro-holes in stainless steel orthopedic implants and surgical instruments.
Locating holes in injection mold and stamping die plates for precise guide-pin fit.
Fluid passage bores in steel valve blocks, sealed for high-pressure systems. Also used in automotive engine and transmission hydraulics.
Send your bore size, tolerance and drawing. We manufacture standard sizes and custom reamers made to your samples or drawings.