American Standard 1/2 blind hole taps
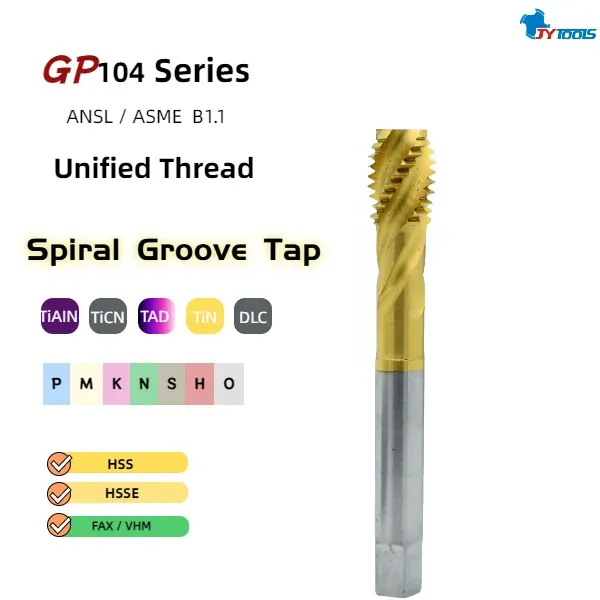
The GP104 is a professional-grade spiral flute tap specifically designed for high-efficiency tapping of ANSI/ASME B1.1 standard threads. It effectively improves machining speed, thread accuracy, and tool life, enhancing both machining efficiency and thread quality while reducing machining costs. It is particularly suitable for applications in the automotive, aerospace, machinery, and hydraulic industries where high metric or imperial thread accuracy is required. It excels in high-efficiency machining and with complex materials. The spiral flute design effectively expels chips upwards (for blind holes) or downwards (for through holes), preventing chip clogging, improving machining efficiency, and reducing thread damage. Suitable for rust-resistant and acid-resistant materials – austenitic stainless steel; ferritic and martensitic stainless steel; pure titanium; nickel alloys; pure copper. Used in tapping spindles with axial compensation (conventional thread cutting) or rigid tapping.
| Part number | GP104E12BSW |
|---|---|
| Material | HSS-E |
| Product Name | American Standard Cutting Taps/Blind Hole Taps |
| OEM / ODM | Made to your samples or drawings |
| Specifications | September 16-18 UNF |
| Lead time | 2 Weeks |
| Packaging (mm) | 15 × 15 × 100L |
| Thread Diameter D1 | 9/16-18UNF |
| Cut-out Length L3 | 30.0mm |
| Shank diameter D | Ø10.5mm |
| Overall Length L | 120.0mm |
| Thread Tolerance Grade ISO | JIS P2 |
| Coating | TiN |
| MOQ | 2 pcs |
| Origin | Shenzhen, China |
Design details engineered for accuracy, tool life and process stability.
Grinded using a high-precision thread grinder, the thread profile accuracy is controlled within ±0.01mm, and the thread surface finish can reach below Ra0.4μm, ensuring the accuracy of ANSI standard threaded connections.
Available in TiAlN, TiCN, TAD, TiN, DLC, and other coatings, with a maximum hardness of HV3400 and a friction coefficient as low as 0.15. Tool life is extended by 2-3 times compared to uncoated taps.
Chip removal direction is opposite to the tapping direction, improving chip removal efficiency by 40% compared to straight flute taps, effectively preventing chip clogging, and is particularly suitable for blind hole tapping.
Suitable for harder materials.
Suitable for processing soft or highly ductile materials.
High-performance helical cutting taps significantly improve production efficiency and quality in applications requiring high machining speed, thread accuracy, and tool life, especially in automated machine tools and CNC machining centers.
Spiral taps are particularly suitable for blind hole machining because chips are expelled upwards along the helical flutes, preventing clogging at the bottom of the hole.
This effectively prevents tap breakage or thread surface defects caused by chip clogging, improving machining reliability.
In blind hole machining, it prevents chip accumulation at the bottom of the hole, improving machining efficiency and quality.
The helical flute structure performs excellently in chip removal and cutting processes in deep threaded holes.
Send the thread standard, size and tolerance class. We supply standard taps and thread mills, plus special threads made to your samples or drawings.