XC Type Carbide Drill
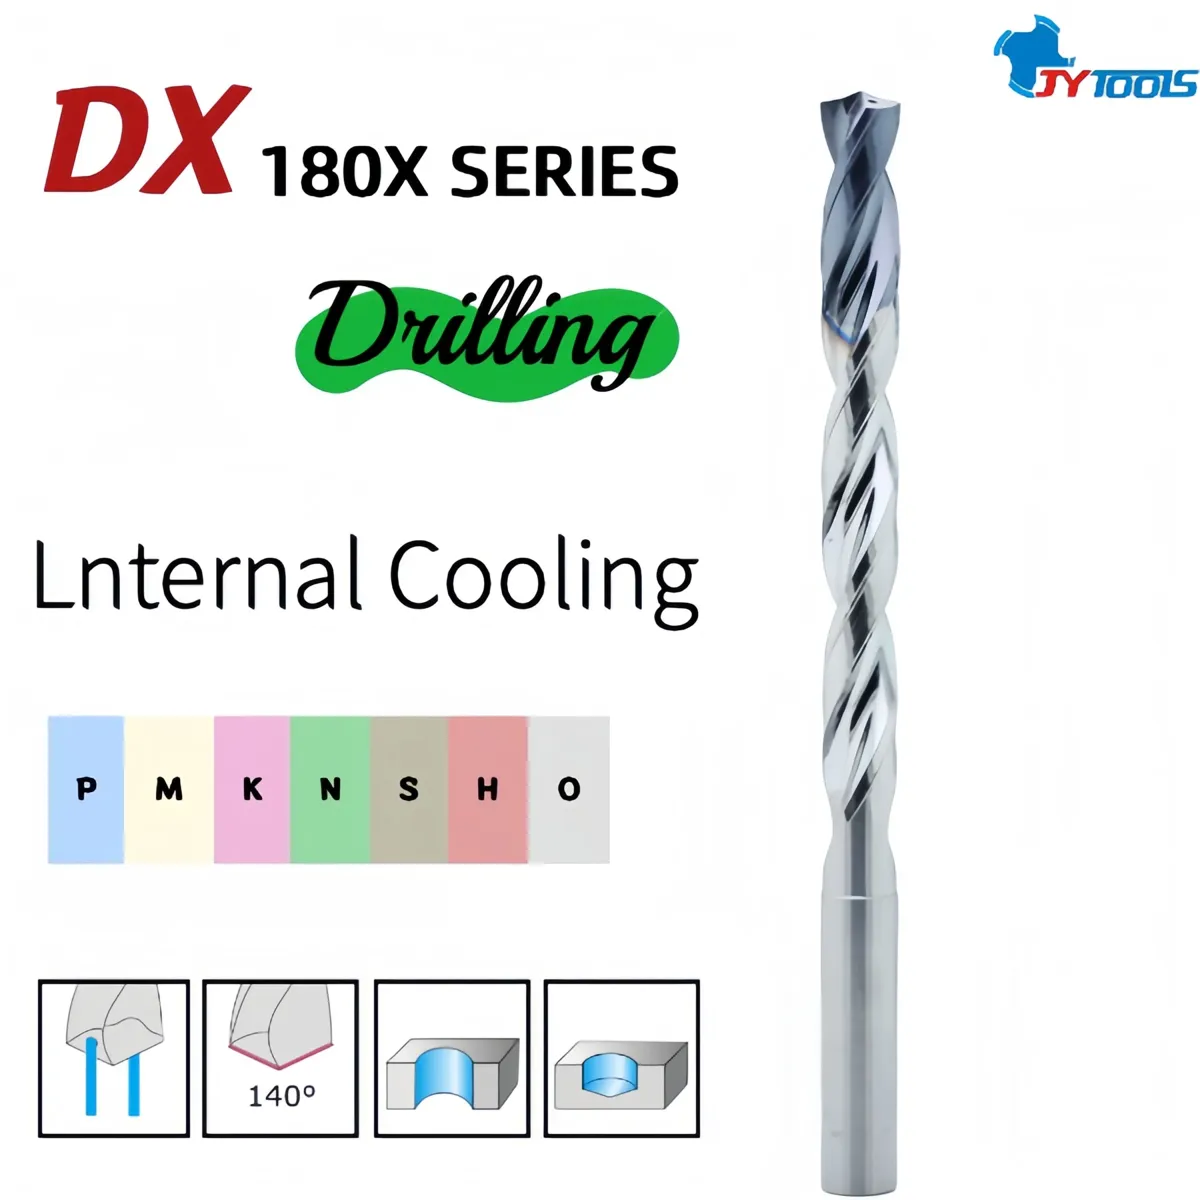
The DX180X series of internally cooled, extra-long-flute carbide drill bits are high-performance tools developed by JIAYI Tools specifically for deep-hole drilling applications (15 times the diameter or more) and difficult-to-machine materials. Their innovative "dual-hole internal cooling + 42° high-helix flute" design, Achieving breakthroughs in deep-hole drilling—including "internal cooling directly to the cutting zone, zero clogging with spiral chip evacuation, and high feed rates without tool burning"—thoroughly resolves the industry pain points associated with traditional deep-hole drills, such as "poor heat dissipation, difficult chip evacuation, and susceptibility to tool burning." It provides disruptive deep-hole drilling solutions for the aerospace, energy equipment, and mold industries.
| Part Number | DX180082X |
|---|---|
| Drill Bit Base Material | Ultrafine-Grained Tungsten Carbide Alloy |
| Product Name | Internally Cooled Carbide Drill Bits/Step Drill Bits |
| OEM / ODM | Made to your samples or drawings |
| Specifications | Ø11.80 × 96L × Ø12.0 × 162L |
| Lead time | 2 weeks |
| Packaging (mm) | 15 × 15 × 200mm |
| Blade Diameter DC | Ø11.8mm |
| Blade Length LCF | 96.0mm |
| Shank Diameter DC | Ø12.0mm |
| Overall length OAL | 162.0mm |
| Materials | VHM (ultrafine-grained tungsten carbide alloy) |
| Coating | AlTiN |
| MOQ | 2 pcs |
| Origin | Shenzhen, China |
Design details engineered for accuracy, tool life and process stability.
The cutter body is machined from a single piece of ultra-fine-grain carbide (HRC 68) with no welded joints, ensuring no loosening or runout during high-speed, high-feed machining, with a repeatability of ≤0.003 mm.
The drill features two built-in high-precision internal coolant channels capable of delivering cooling pressure up to 120 bar. The coolant is directed directly to the cutting edge, improving heat dissipation efficiency by 60% and completely eliminating the risk of drill burnout during deep-hole drilling.
Featuring a 42° high-helix chip-removal flute, chips are naturally discharged upward along the flute, improving chip removal efficiency by 50% during deep-hole machining at 15 times the diameter, thereby preventing chip jams and scratches on the hole walls.
Using PVD nano-coating technology, the coating is only 2 μm thick, with a hardness of up to HV3800 and a coefficient of friction as low as 0.3, resulting in a tool life that is twice as long as that of traditional coatings.
The drill tip features a 140° centering design with a centering accuracy of ≤0.003 mm, allowing for direct machining without the need to pre-drill a center hole, thereby reducing the number of processing steps and improving efficiency.
Each drill bit passes a G2.5-grade dynamic balancing test, ensuring vibration-free operation at high speeds of 20,000 rpm and guaranteeing machining stability.
The cutting edge is ground using a five-axis CNC grinding machine, with a runout error of ≤0.002 mm, ensuring the roundness and cylindricity of the bore.
Pre- and post-polishing processes reduce friction and ensure excellent chip management
Starting values. Our engineers can tune parameters to your machine and workpiece.
| Workpiece material | Cutting speed vc (m/min) | Feed f (mm/rev) | Coolant |
|---|---|---|---|
| 316L Stainless Steel | 50–80 | 0.06–0.15 | Internal + MQL |
| High-temperature alloy Inconel 718 | 30–50 | 0.04–0.1 | High-pressure internal |
| Ti6Al4V titanium alloy | 40–60 | 0.05–0.12 | High-pressure internal |
Typical industries and parts machined with this tool.
Send your hole diameter, depth and workpiece material. We supply standard drills and custom step and special drills made to your samples or drawings.