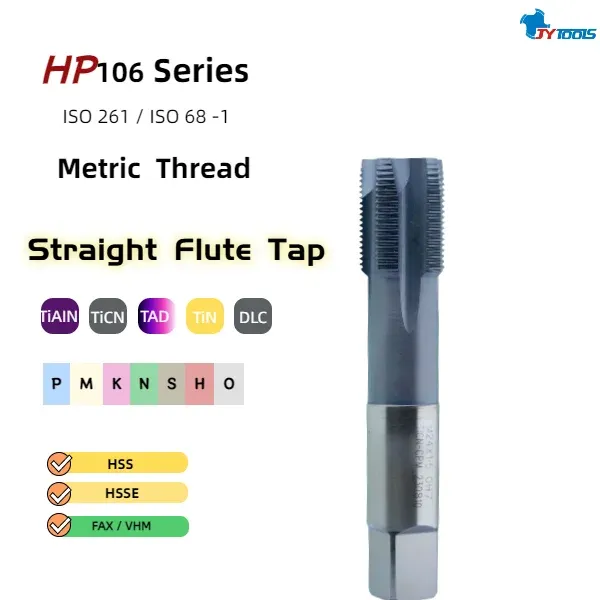
Spiral Point Tap
The HP106 tip tap's main advantages lie in its efficient guiding, excellent thread accuracy, good chip removal performance, and stable machining process. It is particularly suitable for thread machining applications requiring high precision and efficiency, especially with hard materials, precision workpieces, or complex processes, significantly improving machining quality and production efficiency. It is especially suitable for applications in the automotive, aerospace, machinery, and hydraulic industries where high metric or imperial thread accuracy is required. It performs exceptionally well in high-efficiency machining and with complex materials. With repeated use, the tip tap reduces the frequency of tool adjustments and recalibrations, improving machining efficiency and consistency. It reduces vibration during the initial contact of the tap in the hole, ensuring a more precise thread start and reducing machining errors.
| Part number | HP106024M |
|---|---|
| Material | HSS-E-PM |
| Product Name | Metric Cutting Taps |
| OEM / ODM | Made to your samples or drawings |
| Specifications | M24 × 1.5P |
| Lead time | 2 Weeks |
| Packaging (mm) | 30 × 30 × 150L |
| Thread Diameter D1 | M24 × 1.50P |
| Cut-out Length L3 | 45.0mm |
| Shank diameter D | Ø19.0mm |
| Overall Length L | 120.0mm |
| Thread Tolerance Grade ISO | OH7 |
| Coating | TiCN-CPM |
| MOQ | 2 pcs |
| Origin | Shenzhen, China |
Design details engineered for accuracy, tool life and process stability.
Ground using a high-precision thread grinder, the thread profile accuracy is controlled within ±0.01mm, and the thread surface finish can reach below Ra0.4μm, ensuring the accuracy of metric thread connections.
A leading tap (also called a tip tap or pilot tap) is a specially designed tap used in thread cutting, typically in the initial stage of tapping to aid in grinding and guide the entire thread cutting process. Its design and function offer many unique advantages, making it particularly suitable for high-precision, high-efficiency machining requirements.
A leading tap has a special leading section (usually the initial cutting section with a larger helix angle) that helps ensure the tap accurately enters the hole at the start of cutting, preventing deviation.
Considering smooth chip removal, it reduces the possibility of chip accumulation and clogging. Its helical flute design effectively removes chips during cutting, maintaining a smooth machining process.
The design and structure of a tip tap effectively reduce the risk of premature tool wear and breakage, especially during continuous cutting, significantly improving machining stability and tool life.
The leader section design ensures uniform cutting force distribution throughout the thread cutting process, reducing potential vibration and tool deformation.
The tip tap design is used for initial cutting, ensuring precise thread initiation and reducing errors, making it particularly suitable for demanding thread machining tasks.
Tip taps are especially suitable for applications requiring high precision, maintaining high efficiency while ensuring high thread accuracy.
In blind hole machining, it prevents chip accumulation at the bottom of the hole, improving machining efficiency and quality.
The helical flute structure performs excellently in chip removal and cutting processes in deep threaded holes.
Send the thread standard, size and tolerance class. We supply standard taps and thread mills, plus special threads made to your samples or drawings.