UNF American Thread Taps
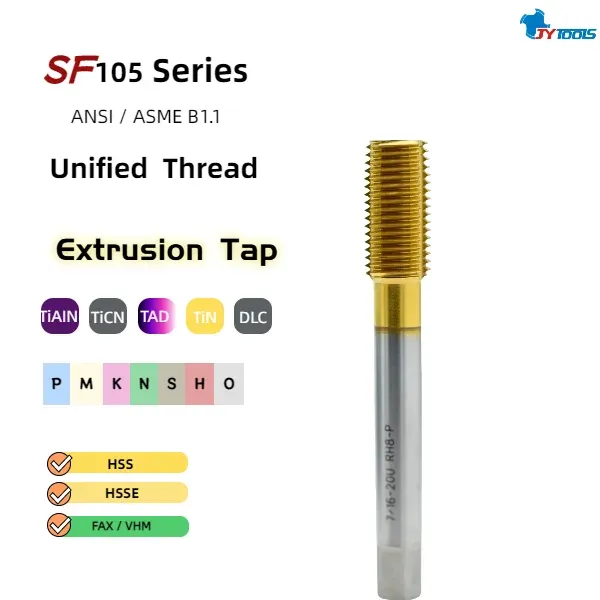
The SF105 forming tap performs cold working on the material during machining, resulting in a denser and smoother thread surface, reducing surface roughness and improving thread performance. It is particularly suitable for thread machining applications requiring high precision and efficiency, especially with hard materials, precision workpieces, or complex processes, significantly improving machining quality and production efficiency. It is especially suitable for applications in the automotive, aerospace, machinery, and hydraulic industries where high precision of metric or imperial threads is required. Its chipless forming, superior wear resistance, and excellent thread strength make it an ideal choice for tapping UNC/UNF/UNEF standard threads on ductile materials such as aluminum alloys, steel, and stainless steel, providing an efficient and stable chipless tapping solution for your precision assembly needs.
| Part number | SF105 |
|---|---|
| Material | HSS / HSS-E / HSS-E-PM |
| Product Name | American Standard Thread Taps/Extrusion Thread Taps |
| OEM / ODM | Made to your samples or drawings |
| Specifications | July 16-20 UN |
| Lead time | 2 Weeks |
| Packaging (mm) | 15 × 15 × 100L |
| Thread Diameter D1 | 7/16-20UN |
| Cut-out Length L3 | 25.0mm |
| Shank diameter D | Ø14mm |
| Overall Length L | 110.0mm |
| Thread Tolerance Grade ISO | 2BX |
| Coating | TiN |
| MOQ | 2 pcs |
| Origin | Shenzhen, China |
Design details engineered for accuracy, tool life and process stability.
Grinded using a high-precision thread grinder, thread profile accuracy is controlled within ±0.01mm, thread surface finish can reach below Ra0.2μm, and thread connection strength is increased by 20% compared to cutting taps.
TiAlN, TiCN, TAD, TiN, DLC, etc., coatings with a maximum hardness of HV3400, a friction coefficient as low as 0.15, and tool life extended by 2-3 times compared to uncoated taps.
Ultra-fine grain carbide substrate, hardness HRC65, 50% improved anti-chipping ability, suitable for tapping difficult-to-machine plastic materials such as stainless steel and high-hardness steel.
High-speed steel (HSS) and high-performance high-speed steel (HSSE) substrates, combining high toughness and red hardness, suitable for tapping general-purpose plastic materials such as aluminum alloys and low-carbon steel.
Threads are formed by plastic deformation of the workpiece material through extrusion, producing no chips and avoiding chip clogging and workpiece scratches. It is especially suitable for tapping blind holes.
A 15° extrusion cone angle achieves progressive plastic deformation, reducing the risk of material cracking and meeting the chipless tapping requirements of ductile materials.
Uses a DIN376 standard square shank, compatible with various tapping chucks, allowing for quick mounting on CNC machining centers, tapping machines, and drilling machines, improving tool change efficiency by 20%.
Extrusion tapping produces no cutting waste, reducing environmental impact and making it more environmentally friendly. In blind hole machining, it prevents chip accumulation at the bottom of the hole, improving machining efficiency and quality.
Send the thread standard, size and tolerance class. We supply standard taps and thread mills, plus special threads made to your samples or drawings.