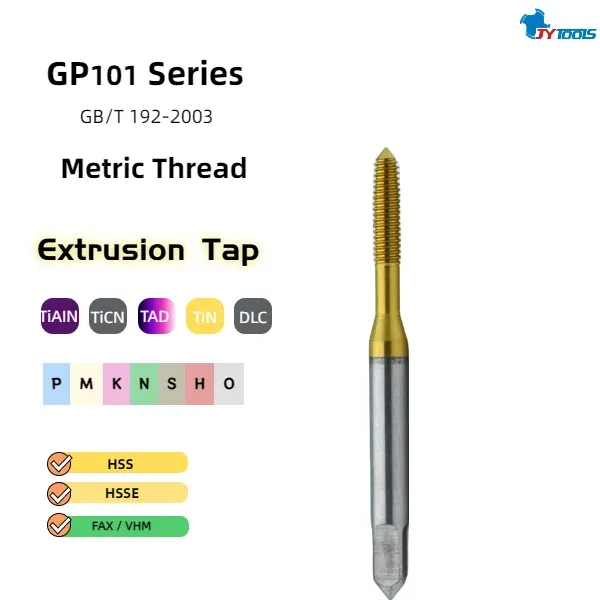
M metric thread tap
The GP101 is a professional-grade forming tap specifically designed for chipless tapping of GB/T 192-2003 standard metric threads (typically used for machining small-diameter threads of the MF (Unified Thread) standard). Its advantages lie primarily in its adaptability, machining accuracy, and reliability, particularly excelling in the production of small parts and precision machining. Small-diameter metric thread taps, with their high precision, high reliability, and high adaptability, are widely used in demanding scenarios involving the machining of small threads. Whether for complex workpieces or automated machining, they effectively improve machining efficiency and quality, making them an indispensable tool in modern manufacturing. They perform exceptionally well in high-efficiency machining and with complex materials. Because there is no cutting process, the threads machined by forming taps are burr-free, making them suitable for workpieces requiring high surface quality.
| Part number | GP101E05MF |
|---|---|
| Material | HSS / HSS-E / HSS-E-PM / VHM |
| Product Name | Metric Thread Taps/Extrusion Thread Taps |
| OEM / ODM | Made to your samples or drawings |
| Specifications | M3.0 × 0.5P |
| Lead time | 2 Weeks |
| Packaging (mm) | 6 × 6 × 60L |
| Thread Diameter D1 | 6-32UN |
| Cut-out Length L3 | 18.0mm |
| Shank diameter D | Ø4mm |
| Overall Length L | 48.0mm |
| Thread Tolerance Grade ISO | RH5 |
| Coating | TiCN |
| MOQ | 2 pcs |
| Origin | Shenzhen, China |
Design details engineered for accuracy, tool life and process stability.
Ground using a high-precision thread grinder, the thread profile accuracy is controlled within ±0.01mm, the thread surface finish can reach below Ra0.2μm, and the thread connection strength is increased by 20% compared to cutting taps.
Ultra-fine grain cemented carbide base material, hardness HRC65, 50% improved resistance to chipping, suitable for tapping difficult-to-machine plastic materials such as stainless steel and high-hardness steel.
TiAlN, TiCN, TAD, TiN, DLC, etc., with coating hardness up to HV3400 and a friction coefficient as low as 0.15, extending tool life by 2-3 times compared to uncoated taps.
Threads are formed by plastic deformation of the workpiece material through extrusion, generating no chips and avoiding chip clogging and workpiece scratches, making it particularly suitable for blind hole tapping.
Such as instruments and meters, micro pumps, etc.
Forming taps hold a vital position in modern manufacturing due to their advantages such as high-quality thread formation, increased strength, long tool life, and chip-free machining. They are particularly advantageous in scenarios requiring high efficiency, environmental friendliness, and high precision machining.
The structure designed specifically for small diameters distributes cutting forces more evenly, reducing the risk of tap breakage due to stress concentration.
In blind hole machining, it prevents chip accumulation at the bottom of the hole, improving machining efficiency and quality.
Extrusion tapping produces no cutting waste, reducing environmental impact and making it more environmentally friendly.
Small diameter metric thread taps are suitable for the following scenarios.
Machining of casings and connectors for small electronic components.
Machining of tiny threads in precision medical equipment.
Machining small components with high precision requirements.
Send the thread standard, size and tolerance class. We supply standard taps and thread mills, plus special threads made to your samples or drawings.